Home / Products / Waste Heat Recovery
Waste Heat Recovery
Boiler Economizer
Recover boiler flue-gas heat for feedwater, air and process-water heating.
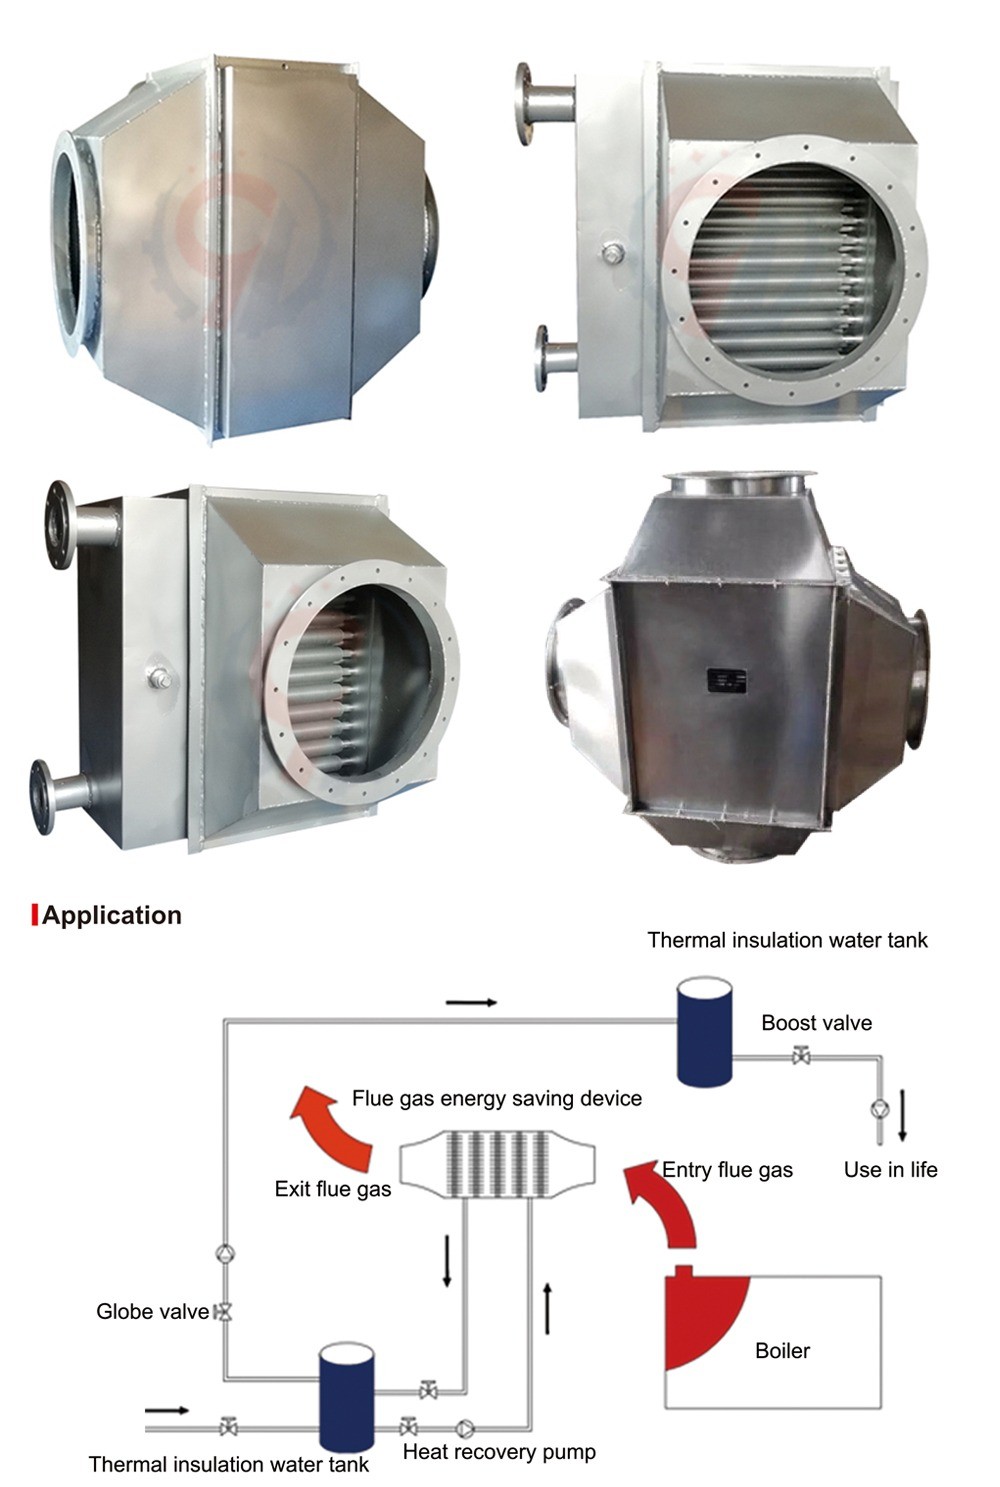
A significant amount of energy leaves an industrial boiler through hot flue gases. Engineered economizer solutions recover useful thermal energy for boiler feedwater preheating, combustion-air preheating, process-water heating and hot-water generation.
Customized retrofit and OEM replacement options support lower stack temperatures and reduced fuel consumption. Materials and thermal design are selected for each application.
Specifications
| Technology partners | Hylita and Qingli Heat Exchanger |
|---|---|
| Heat transfer area | 5–500 m² |
| Airflow capacity | 500–50,000 m³/h |
| Air pressure drop | 50–300 Pa |
| Materials | Carbon steel, SS304/316L, copper, aluminium, Corten steel or titanium |
| Design selection | Subject to duty, fluid compatibility, corrosion and operating conditions |
Technology in focus
Related Technology & Applications
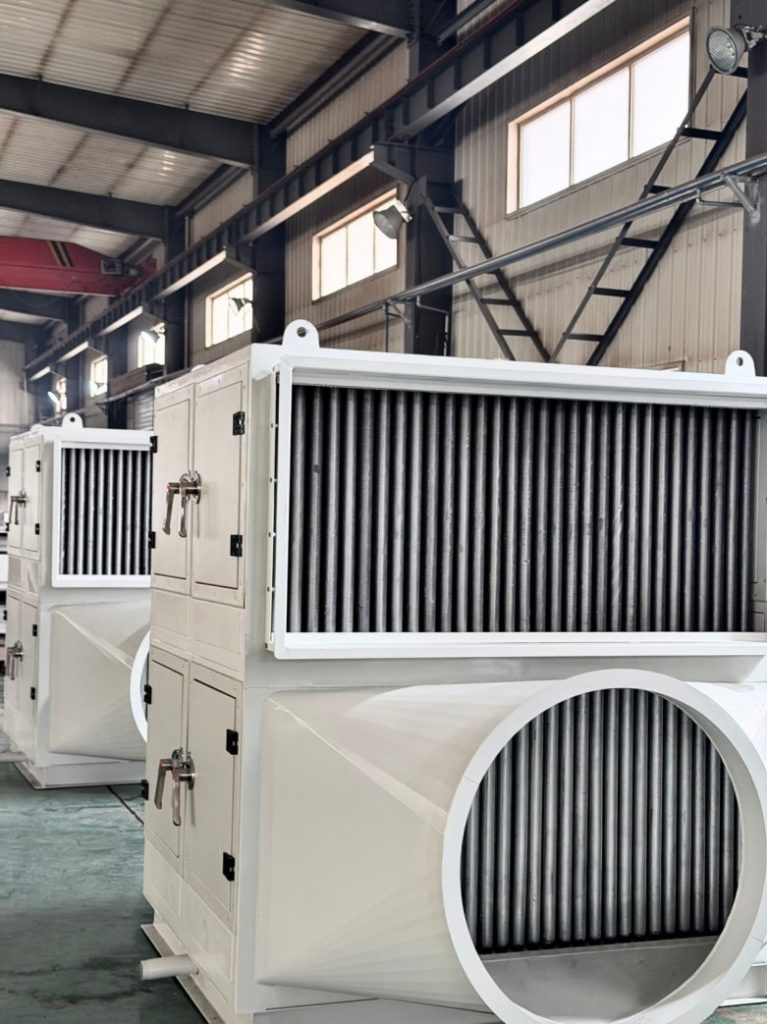
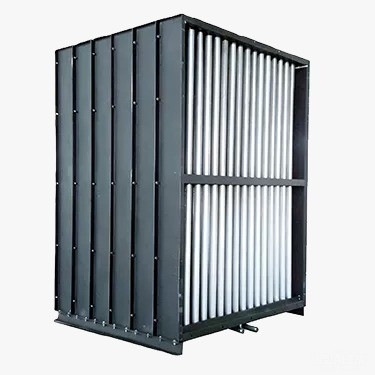
Application reference images. Equipment shown may differ from the selected model and project configuration.